양면 전기접점 제작: 리벳팅 체결과 뒤쪽 접촉면 성형
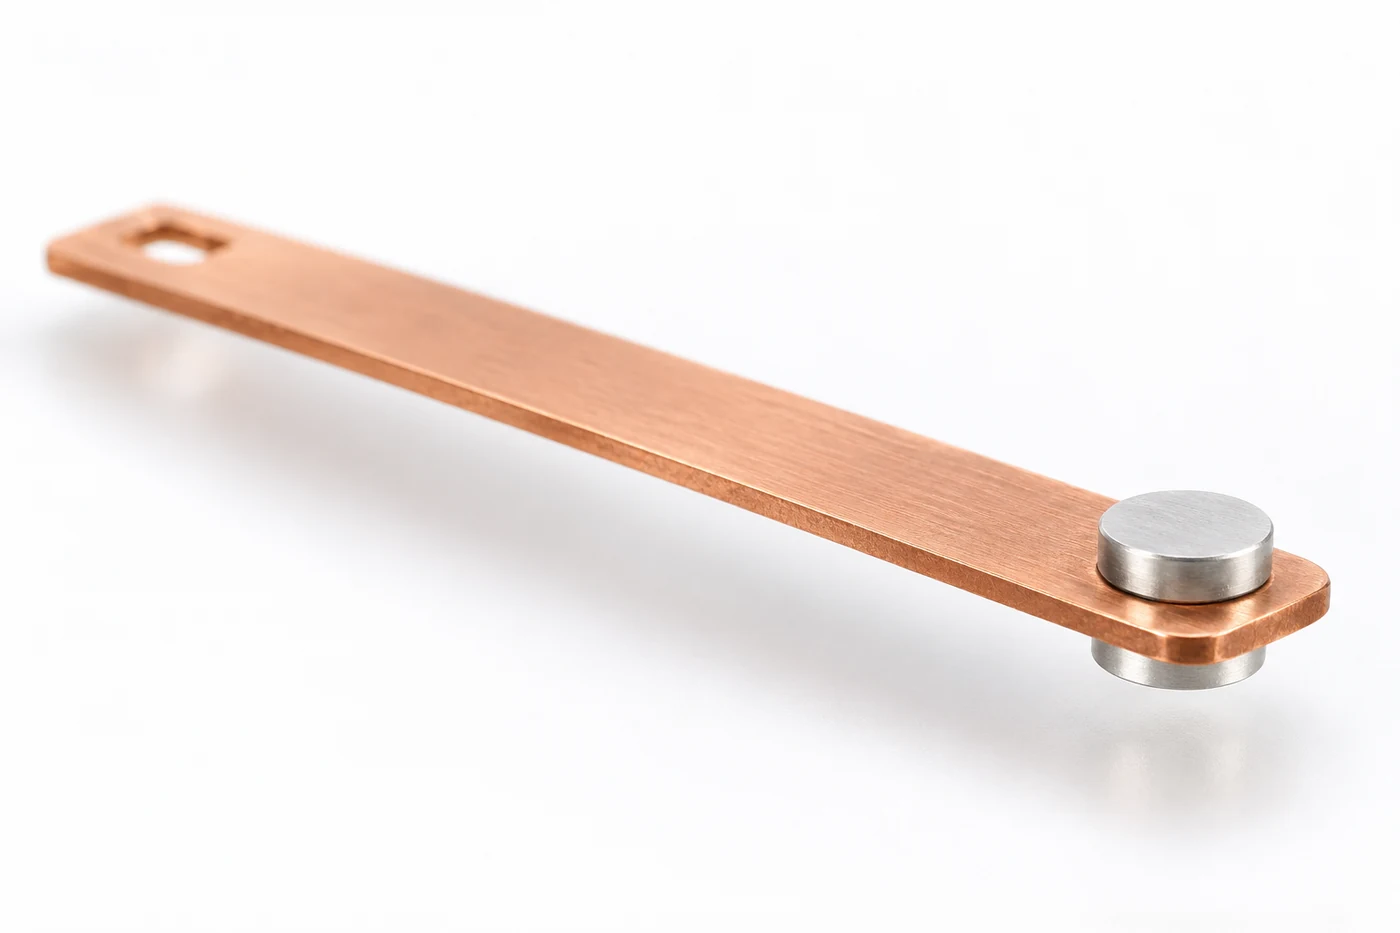
양면 전기접점은 접점 다리를 가동편 뒤쪽에서 리벳팅해 단단히 체결하는 동시에, 성형된 뒤쪽 머리까지 접촉면으로 사용하는 부품입니다. 앞뒤 접촉 기능을 안정적으로 만들려면 접점 재료의 배치부터 다리의 금속 유동, 가동편 변형, 접촉 높이와 전기적 검사까지 함께 설계해야 합니다.
전기접점과 프레스 가동편이 만나는 이 구조의 핵심은 작은 체결부 안에 있습니다. 후면 머리는 부품을 붙잡는 역할과 전류를 전달하는 역할을 함께 수행하므로, 조립 품질이 곧 접촉 품질로 이어집니다.
01리벳팅으로 완성되는 앞뒤 두 접촉면
양면 전기접점은 가동편의 한쪽에 놓인 접점 머리와 반대쪽으로 돌출된 다리를 하나의 부품으로 연결한 구조입니다. 다리를 가동편의 구멍에 끼운 뒤 압축 성형하면 뒤쪽 재료가 옆으로 퍼지면서 제2의 머리가 만들어집니다. 이 머리가 가동편을 붙잡는 체결부이자 반대편 고정접점과 맞닿는 접촉면으로 작동합니다. 뒤쪽 리벳팅 형상이 곧 전기적 기능면이 된다는 점이 일반 체결용 리벳과의 핵심 차이입니다.
전면 머리는 처음부터 준비된 접촉 형상이고, 후면 머리는 조립 공정에서 완성되는 접촉 형상입니다. 따라서 앞면의 치수만 맞추거나 뒤쪽을 충분히 퍼뜨리는 것만으로 품질을 판단할 수 없습니다. 앞면을 손상시키지 않으면서 뒤쪽 높이·외경·면 상태를 확보하고, 그 사이에서 가동편의 평탄도와 탄성 특성을 유지해야 합니다.
| 구성 부위 | 기계적 역할 | 전기적 역할 |
|---|---|---|
| 전면 접점 머리 | 초기 위치 결정과 성형 중 지지 | 한쪽 상대 접점과의 접촉 |
| 관통 다리 | 구멍을 통한 연결과 성형 재료 공급 | 접점 머리와 가동편 사이의 전류 경로 구성 |
| 후면 성형 머리 | 가동편을 붙잡는 체결부 형성 | 반대쪽 상대 접점과의 접촉 |
| 프레스 가동편 | 접점 위치와 작동 변위·접촉력 제공 | 외부 단자에서 접점으로 이어지는 통전 경로 |
전환형 기구에서는 가동편의 이동에 따라 앞면과 뒷면이 각기 다른 고정접점에 닿을 수 있습니다. 실제 통전 순서와 개폐 기능은 기구·회로 구성으로 결정됩니다. 양면 구조만으로 양쪽이 동시에 통전하거나, 자동으로 이중 차단 기능을 갖는 것은 아닙니다.
02후면 접촉 기능을 결정하는 재료 배치
뒤쪽을 성형해 접촉면으로 사용하려면 그 위치에 필요한 접점 재료가 확보되어야 합니다. 솔리드 접점은 머리와 다리가 동일한 접점 재료로 이어져 있어 다리 끝을 성형한 뒤에도 해당 재료가 후면을 구성합니다. 다만 같은 재료라도 가공경화와 성형 이력이 다르므로 앞뒤 경도와 표면 상태까지 같다고 볼 수는 없습니다.
일반적인 단면 클래드 접점은 머리의 접촉층에 귀금속 재료를 사용하고, 나머지 몸체와 다리는 동 또는 동합금으로 구성합니다. 이 다리를 뒤쪽에서 리벳팅하면 후면은 기본적으로 다리 재료의 표면입니다. 은계 접촉층이 자동으로 생기거나 앞면과 같은 개폐 성능을 갖는 것은 아닙니다. 후면을 전기접점으로 사용할 때는 그 재질과 상대 접점의 조합을 별도로 선정해야 합니다.
재료 구성과 성형 후 기능층
| 재료 구성 | 뒤쪽 성형 후의 검토점 | 설계의 중심 |
|---|---|---|
| 솔리드 접점 | 동일 접점 재료의 성형성·경화·균열 | 필요한 접점 특성과 조립 가공성의 균형 |
| 단면 클래드 접점 | 후면에 노출되는 다리 재료의 접촉 적합성 | 앞면 접촉층과 후면 기능의 구분 |
| 양단 접점 재료를 갖는 복합 구조 | 성형 후 후면 기능층의 연속성과 잔여 두께 | 재료 배치와 성형 유동을 함께 설계 |
양면용 복합 접점은 머리와 다리 끝에 각각 필요한 접점 재료를 배치하고, 중간을 동계 재료로 구성하는 방식도 사용합니다. 중요한 것은 성형 전 소재 단면만이 아니라 후면 머리까지 만든 뒤 실제 접촉 위치에 어떤 재료가 얼마나 연속적으로 남는지입니다.
AgCu, AgNi 등 은계 재료도 합금·복합 구조, 조성, 가공 상태에 따라 성형성과 접촉 특성이 달라집니다. 재료 이름 하나로 성형 하중이나 완성 형상을 고정하지 않습니다. 통전·개폐 조건에 맞는 접점 재료를 먼저 검토하고, 그 재료로 안정적으로 후면 머리를 만들 수 있는 공정 조건을 연결해야 합니다.
03다리 돌출량과 가동편 구멍의 준비
후면 머리를 만드는 재료는 가동편 밖으로 돌출된 다리에서 공급됩니다. 돌출량이 부족하면 목표 접촉 높이와 체결 형상을 함께 확보하기 어렵고, 과도하면 큰 압축 변형과 불안정한 퍼짐이 발생할 수 있습니다. 다리 길이는 가동편의 판두께, 구멍 안으로 채워지는 양, 목표 후면 형상을 함께 고려해 정해야 합니다.
가동편 구멍의 직경과 형상도 공정의 일부입니다. 구멍과 다리의 조합은 삽입성, 초기 동심도, 성형 중 구멍 채움, 체결부의 유격에 영향을 줍니다. 한쪽으로 찌그러진 구멍이나 거친 파단면은 다리를 기울게 하거나 국부적인 재료 유동을 만들 수 있습니다. 구멍 주변의 버는 접점 머리의 안착을 방해하고 가동편에 불균일한 하중을 전달합니다.
| 관리 항목 | 조립에서 나타나는 영향 | 확인 방법 |
|---|---|---|
| 다리 길이와 돌출량 | 후면 높이·외경·성형 여유 | 입고 치수와 가동편 조립 상태의 돌출량 확인 |
| 가동편 판두께 | 돌출량과 체결 간격 변화 | 기능부 주변의 실제 두께와 편차 확인 |
| 구멍 크기·진원도·위치 | 삽입성·동심도·국부 유동 | 구멍과 외곽 기준의 관계 확인 |
| 버·전단면·표면 오염 | 안착 불량·긁힘·접합부 저항 변화 | 앞뒤 가장자리와 접촉 계면 확인 |
이 단계에서는 프레스 가공과 접점 조립을 분리해서 판단하지 않는 것이 좋습니다. 구멍 위치가 맞아도 가동편에 휨이 남아 있으면 성형 공구의 축과 접점 축이 어긋날 수 있습니다. 조립 지그는 단순히 부품을 잡는 장치가 아니라, 가동편의 기준면과 접점 위치를 반복해서 재현하는 기준계 역할을 해야 합니다.

04삽입·지지·성형·해제로 이어지는 리벳팅 공정
양면 전기접점의 조립은 접점 삽입, 전면 지지, 후면 성형, 하중 해제 후 확인의 순서로 이해할 수 있습니다. 공정의 출발점은 이미 완성된 전면 접촉면을 보호하는 일입니다. 지지 공구는 머리의 형상과 맞고 충분한 강성을 가져야 하며, 접촉면에 찍힘이나 미세한 기울어짐을 남기지 않아야 합니다.
| 공정 | 핵심 제어 | 공정 이후의 확인 |
|---|---|---|
| 삽입과 위치 결정 | 다리·구멍의 정렬과 전면 안착 | 들뜸·기울어짐·돌출량 |
| 전면 지지 | 머리 형상에 맞는 지지와 공구 청결 | 접촉면 압흔과 지지 불균일 |
| 후면 업세팅 | 정해진 변형 경로와 공구 정렬 | 후면 높이·외경·편심·균열 |
| 해제와 배출 | 지그 하중 제거와 변형 복귀 | 가동편 휨·접점 위치·잔류 유격 |
직선 가압, 궤도 리벳팅 등 성형 방식은 재료와 부품 구조에 맞춰 선택합니다. 궤도 리벳팅은 공구가 접촉하는 영역을 순차적으로 이동시키며 성형하는 방식이며, 얇은 접점 가동편의 변형을 줄이기 위한 선택지로 사용됩니다. 이때 측방력에 대응하는 지지가 필요하고, 복합 접점은 기능층과 몸체 사이 계면의 건전성도 확인해야 합니다. 하중이 낮다는 이유만으로 모든 접점에서 균열과 박리가 방지된다고 판단하지 않습니다.
성형 중 공구 아래에서 평평해 보이던 부품도 하중을 해제하면 잔류응력 때문에 휨이 나타날 수 있습니다. 따라서 가압 종료 시점의 위치만으로 완성 치수를 판정하지 않습니다. 배출 후 안정된 상태의 접점 높이와 가동편 형상을 기준으로 검사 체계를 구성합니다.
05금속 유동과 후면 머리의 형상 제어
업세팅은 다리를 축 방향으로 줄이면서 재료를 옆으로 이동시키는 소성가공입니다. 후면 머리가 넓어지는 동안 일부 재료는 구멍 안쪽이나 접점과 가동편 사이의 공간으로 이동할 수 있습니다. 따라서 같은 돌출 길이와 같은 공구 이동량이라도 소재 경도, 마찰, 구멍 조건, 공구 형상에 따라 최종 높이와 외경이 달라질 수 있습니다.
다리의 재료량은 목표 형상을 만드는 출발점이고, 실제 퍼지는 경로는 공정이 결정합니다. 후면 머리의 외경만 맞추면 가장자리가 얇아지거나 중앙이 오목해진 상태를 놓치기 쉽습니다. 접촉 기능을 갖는 중앙 영역과 가동편을 붙잡는 외곽 영역을 함께 보면서 높이, 단면 형상, 편심, 재료의 연속성을 관리해야 합니다.
후면 성형 형상을 바꾸는 요인
| 변화 요인 | 관찰 가능한 변화 | 검토 방향 |
|---|---|---|
| 소재 경도·가공 이력 | 성형 하중과 퍼짐의 변화 | 입고 상태와 성형 결과 연결 |
| 공구 정렬과 접촉 조건 | 편심·기울어진 머리·국부 얇아짐 | 공구 축과 지그 기준 확인 |
| 마찰과 표면 상태 | 비대칭 유동·표면 뜯김 | 윤활·청정·공구 마모 조건 관리 |
| 성형량과 다리 재료량 | 접촉 높이·외경·체결 형상 변화 | 치수와 하중 이력의 동시 검토 |
복합 재료에서는 금속 유동이 접촉층 분포까지 바꿉니다. 다리 끝의 기능층이 넓어지는 과정에서 국부적으로 얇아지거나 가장자리로 치우칠 수 있으므로, 겉모양이 평평하다는 이유만으로 재료 배치가 적합하다고 판단하지 않습니다. 개발 단계의 단면 확인은 완성 형상과 기능층의 관계를 이해하는 데 도움이 됩니다.
화살표 키로 시점 조절
공구를 분리하면 가동편 양쪽에 기능면이 남습니다. 뒤쪽의 높이·평탄도·균열과 앞쪽의 눌림을 함께 확인합니다.
접점 다리를 뒤쪽에서 압축·확장하여 체결과 후면 접촉면을 함께 만드는 과정
06앞면 보호와 후면 접촉면을 만드는 공구
앞면 지지 공구와 뒤쪽 성형 공구는 한 쌍으로 설계해야 합니다. 앞쪽은 리벳팅 반력을 받아 전면 머리의 변형을 억제하고, 뒤쪽은 기능면의 높이와 형상을 만듭니다. 지지 면의 작은 이물이나 손상도 이미 완성된 접촉면에 전사될 수 있어, 공구의 표면 상태와 세척 주기가 제품 형상만큼 중요합니다.
후면 접촉면의 평탄도와 기울기는 공구 형상, 공구 축, 가동편 기준면의 관계에서 결정됩니다. 접촉면이 가동편에 대해 기울어지면 상대 접점과 한쪽 가장자리부터 닿을 수 있습니다. 이때 접촉 흔적이 치우치고 실제 접촉 영역의 변화가 커질 수 있으므로, 외경 측정에 더해 접촉면 방향과 위치를 확인합니다.
| 공구·지그 항목 | 목적 | 점검 포인트 |
|---|---|---|
| 전면 머리 지지 | 기존 접촉면과 외형 보호 | 형상 적합성·압흔·이물 |
| 후면 성형 면 | 접촉 높이와 접촉면 형상 형성 | 마모·뜯김·표면 전사 |
| 공구 축 정렬 | 편심과 한쪽 퍼짐 억제 | 다리 축·가동편 구멍과의 관계 |
| 가동편 받침 | 주변 판재의 국부 변형 제어 | 지지 위치·평탄도·배출 후 휨 |
성형한 뒤 접촉면을 추가 가공하는 공정이 필요하다면 그 제거량도 처음부터 재료 배치에 포함해야 합니다. 특히 복합 접점은 가공으로 기능층을 지나치게 제거하면 표면의 재질이 달라집니다. 성형, 후가공, 세척, 최종 검사 순서를 따로 정하지 말고 하나의 공정 사양으로 연결하는 것이 중요합니다.
07가동편의 평탄도와 탄성을 지키는 체결
후면 머리를 크게 퍼뜨릴수록 체결이 무조건 좋아지는 것은 아닙니다. 과도한 변형은 구멍 주변 판재를 끌어당기거나 눌러 가동편을 휘게 만들 수 있습니다. 반대로 안착이 부족하면 접점이 미세하게 움직이거나 기울어져 작동 위치와 통전 경로가 불안정해질 수 있습니다. 접촉 기능과 체결 기능을 함께 만족하는 공정 범위를 정해야 합니다.
프레스 가동편은 접점을 지지하는 동시에 스프링 역할을 하는 경우가 많습니다. 리벳팅 부근의 국부 변형이 작아 보여도 가동편 길이 방향의 자세를 바꾸면 실제 조립 상태에서 접촉력이나 전환 위치가 달라질 수 있습니다. 단품 외형 검사에 더해, 가동편의 기능 기준을 유지한 상태에서 접점 높이와 작동 변위를 연결해 확인하는 이유입니다.
성형 하중, 체결 유지 성능, 사용 중 접촉력은 서로 다른 항목입니다. 성형 하중은 조립할 때 다리를 소성변형시키는 힘이고, 체결 유지 성능은 조립 후 접점이 가동편에 얼마나 안정적으로 유지되는지에 관한 특성입니다. 접촉력은 실제 작동 중 상대 접점과 누르는 힘으로, 가동편의 스프링 특성과 기구 변위가 결정합니다. 큰 성형 하중을 그대로 높은 접촉력이나 낮은 접촉 저항으로 해석해서는 안 됩니다.
| 부족 또는 과다 상태 | 가능한 영향 | 기능 확인 |
|---|---|---|
| 머리 안착 부족 | 미세 유격·회전·접합부 저항 변동 | 체결 안정성과 경로 저항 |
| 구멍 주변 과도한 변형 | 가동편 휨·국부 손상 | 자유 상태 평탄도와 조립 위치 |
| 접점 편심·기울어짐 | 한쪽 접촉·접촉 흔적 편중 | 상대 접점과의 정렬 |
| 가동편 탄성 특성 변화 | 접촉력·작동 변위 변화 | 기구 상태별 힘과 위치 |
체결력을 확인하는 인장·밀어냄·회전 저항 등의 시험은 구조와 사용 하중에 맞춰 선택합니다. 서로 다른 시험의 값은 같은 의미가 아니며, 파괴 시험 결과만으로 전기적 접촉 안정성을 대신할 수 없습니다. 기계적 유지 성능과 전기적 기능을 서로 연결하되 각각의 합격 기준을 분명히 두어야 합니다.
08후면 성형면의 균열·접힘·표면 상태
뒤쪽 머리는 큰 소성변형을 거친 기능면입니다. 가장자리 균열, 접힌 재료, 표면 뜯김, 공구 자국, 성형 잔류물은 체결 외관의 문제를 넘어 실제 접촉 위치와 전류 경로에 영향을 줄 수 있습니다. 특히 가장자리의 작은 균열은 위에서 내려다본 사진만으로 놓치기 쉬워, 측면과 경계부를 함께 확인해야 합니다.
접촉면이 눈에 잘 띄게 매끄럽다고 해서 전기적 상태가 항상 좋은 것은 아닙니다. 표면 피막과 유기 잔류물은 낮은 에너지의 신호 접촉에서 저항 변동을 만들 수 있고, 부착 입자는 접촉 흔적과 국부 하중 분포를 바꿀 수 있습니다. 공정 윤활이 필요하더라도 최종 접촉면의 요구 청정도와 호환되는 세척·관리 방식이 함께 있어야 합니다.
| 검사 대상 | 기술적 의미 | 보완 확인 |
|---|---|---|
| 후면 가장자리 균열 | 성형 여유 또는 재료 상태의 한계 신호 | 확대 관찰과 필요한 단면 분석 |
| 접힘·겹침·뜯김 | 불안정한 재료 유동과 표면 결함 | 공구 상태 및 성형 조건 대조 |
| 기능층 단절·기재 노출 | 접촉 위치의 재질 변화 | 재료 분포와 단면 확인 |
| 유분·이물·변색 | 접촉 계면의 상태 변화 | 청정도와 전기적 기능 검사 |
도금이나 표면 처리 여부는 별도의 설계 조건입니다. 도금된 소재를 성형하면 변형부의 표면층 상태를 확인해야 하고, 성형 후 도금하는 방식은 완성 치수와 접촉면 상태를 다시 검토해야 합니다. 도금층을 두껍게 하거나 표면을 광택 처리하는 것만으로 성형 결함이나 내부 체결 불량을 해결할 수는 없습니다.

09앞뒤 접촉 높이와 접촉력의 조합
양면 전기접점은 하나의 부품이지만 앞뒤 접촉 조건은 각각 존재합니다. 전면 높이, 후면 높이, 가동편 위치, 상대 고정접점의 높이와 기울기가 합쳐져 실제 접촉 시점과 눌림량을 만듭니다. 후면 리벳팅 높이의 편차가 커지면 체결은 유지되더라도 한쪽의 접촉력이 달라질 수 있습니다.
접촉력은 눈에 보이는 접점 면적 전체에 균일하게 작용하지 않습니다. 실제 전류는 미세한 접촉 지점을 통해 흐르며, 표면 거칠기·피막·재료·하중의 영향을 받습니다. 따라서 접점 머리를 크게 만드는 설계와 충분한 실제 접촉을 만드는 설계는 구분해서 검토해야 합니다. 접촉력과 면 정렬을 함께 관리하는 이유도 여기에 있습니다.
| 앞뒤로 구분할 항목 | 확인 목적 | 같이 볼 조건 |
|---|---|---|
| 접촉면 높이·위치 | 정해진 작동 위치에서의 접촉 확보 | 가동편과 고정접점의 기준 |
| 면 기울기·접촉 흔적 | 접촉 편중과 가장자리 접촉 확인 | 기구 정렬과 가동편 자세 |
| 접촉력·눌림량 | 통전 안정성과 작동 여유 | 스프링 특성과 조립 공차 |
| 개방 거리·전환 위치 | 기구의 의도한 개폐 순서 확인 | 구동 변위와 전체 회로 구성 |
앞뒤가 같은 재료라도 사용 빈도와 개폐 부하가 다르면 마모와 표면 변화의 진행도 달라질 수 있습니다. 초기 조립에서 양쪽 저항이 비슷하다는 사실만으로 수명 중 상태가 같다고 판단하지 않습니다. 각 면이 맡는 실제 작동 조건을 나누어 평가해야 합니다.
화살표 키로 시점 조절
가동편이 이동하는 동안 두 상대 접점과 간격을 둡니다. 접촉 순서와 개방 간격은 실제 기구 설계에 맞춰 정합니다.
하나의 가동편에서 앞뒤 접촉면이 각각 상대 고정접점과 맞닿는 구조
10통전·발열·개폐 내구성으로 이어지는 접점 품질
통전 상태의 전압 강하는 상대 접점과 맞닿는 계면뿐 아니라 접점 몸체, 가동편과의 연결부, 가동편 자체의 영향을 함께 받습니다. 특정 구간의 저항이 증가하면 해당 구간의 발열이 커질 수 있으며, 온도 상승은 다시 가동편의 접촉력과 표면 상태에 영향을 줄 수 있습니다. 전기적 품질을 접점 재료의 전도율 하나로 설명하기 어려운 이유입니다.
개폐 중에는 접촉 저항 외에 바운스, 아크, 재료 전이, 침식, 융착 가능성도 검토해야 합니다. 이 거동은 전류와 전압만이 아니라 AC/DC, 부하 특성, 작동 속도, 개방 거리, 접촉력 및 상대 접점 재료에 따라 달라집니다. 양면 접점의 재료와 후면 형상은 실제 기구의 전기적 사용 조건과 함께 선정합니다.
| 운전 상태 | 주요 확인 항목 | 평가의 관점 |
|---|---|---|
| 낮은 에너지의 신호 접촉 | 접촉 저항의 안정성과 변동 | 피막·이물·접촉력의 영향 |
| 연속 통전 | 전압 강하와 온도 상승 | 전체 경로와 국부 발열 구분 |
| 반복 개폐 | 바운스·침식·재료 전이·융착 | 실제 부하와 작동 조건 반영 |
| 장기 사용 및 환경 노출 | 저항 변화·접촉력 변화·표면 변질 | 기계·열·환경 영향을 함께 검토 |
재료의 내융착성이 좋다고 해서 접촉력 부족이나 기구의 바운스를 보완할 수 있는 것은 아닙니다. 반대로 단단히 체결된 접점이라도 전류가 통하는 계면에 문제가 있으면 안정적인 접촉을 유지하기 어렵습니다. 재료, 리벳팅 품질, 가동편 특성, 기구 조건을 하나의 작동계로 검증해야 합니다.
11앞면·뒷면·체결부를 나누는 검사 체계
검사는 앞면 접촉 기능, 뒷면 접촉 기능, 가동편과의 체결 기능으로 구분하면 누락을 줄일 수 있습니다. 같은 시험 한 번으로 세 기능을 모두 확인하려고 하면 체결부 저항과 상대 접점의 접촉 저항이 섞이거나, 한쪽 접촉면의 결함이 반대쪽 결과에 가려질 수 있습니다.
전기 저항 측정은 측정점과 전류 경로를 먼저 정해야 합니다. 4선식 측정은 측정 리드의 영향을 줄이지만, 두 감지점 사이에 있는 가동편·체결 계면·상대 접점의 저항은 여전히 결과에 포함됩니다. 따라서 전체 경로의 값인지 특정 구간의 값인지 구분하고, 앞뒤 비교에서는 프로브의 재료와 위치, 접촉력, 하중 이력을 일정하게 관리합니다. 저에너지 접촉을 평가할 때는 시험 전류와 전압이 표면 피막을 변화시키지 않도록 목적에 맞는 조건을 사용합니다.
| 검사 구분 | 확인 내용 | 기록해야 할 조건 |
|---|---|---|
| 형상 검사 | 앞뒤 높이·외경·기울기·가동편 휨 | 기준면과 하중 해제 상태 |
| 표면·재료 검사 | 균열·접힘·기능층 분포·잔류물 | 관찰 위치와 검사 방법 |
| 체결 검사 | 유격·회전·유지 성능 | 하중 방향·지지 조건·판정 기준 |
| 전기 검사 | 각 면의 저항·전압 강하·발열 | 측정점·접촉력·전류·시간 |
| 작동 내구 검사 | 개폐 후 저항·마모·접촉력 변화 | 부하·작동 속도·평가 시점 |
개발 단계에서는 단면 분석과 파괴 시험으로 형상과 내부 상태의 관계를 확인하고, 양산에서는 반복 가능한 비파괴 치수·외관·전기 검사와 공정 감시를 조합할 수 있습니다. 모든 제품에 같은 검사 항목과 빈도를 적용하기보다, 고장 영향과 공정 변동을 기준으로 검사 계획을 정합니다.
12성형 이력과 완성 품질을 연결하는 공정 관리
리벳팅 장비의 설정값만 같아도 소재와 부품 상태가 달라지면 결과는 달라질 수 있습니다. 접점의 가공 상태, 가동편 두께, 구멍 품질, 공구 마모, 지그 오염을 완성 치수와 함께 기록하면 원인 추적이 쉬워집니다. 특히 후면 접촉 높이는 체결부의 형상인 동시에 기구의 기능 치수이므로 공정 관리에서 우선순위가 높습니다.
장비가 지원하는 경우 하중·변위 이력은 잘못된 삽입, 재료량 변화, 비정상적인 성형 저항을 찾는 데 도움이 됩니다. 다만 정상 범위의 파형이 표면 청정도나 내부 기능층 상태까지 보증하지는 않습니다. 공정 이력은 실제 치수·단면·기능 검사와 연결해 관리 한계를 정할 때 가치가 있습니다.
공정 기록과 완성품 품질의 연결
| 공정 관리 대상 | 함께 연결할 결과 | 변경 시 확인 |
|---|---|---|
| 접점 소재 로트와 가공 상태 | 성형 하중·균열·접촉면 상태 | 재료 변경 전후의 성형·기능 비교 |
| 프레스 가동편 로트 | 돌출량·가동편 휨·접촉 위치 | 판두께·구멍·표면 상태 |
| 공구 수명과 유지보수 | 높이·편심·표면 전사 | 교환 직후 초품과 재현성 |
| 가압 조건과 지그 상태 | 체결 형상·유격·전기적 변동 | 조건 변경 이력과 기능 확인 |
불량을 뒤쪽 외관 문제로만 분류하면 앞면 지지 불량이나 프레스 구멍 문제를 놓칠 수 있습니다. 제품의 어느 면에 증상이 나타났는지와 실제 원인이 생긴 공정은 다를 수 있습니다. 앞뒤 사진, 치수, 성형 이력, 검사 결과를 같은 부품 식별 정보에 연결하는 방식이 효과적입니다.
양면 접점의 접촉면·체결부·가동편 검사 연결도
13제작 도면과 검사 기준을 완성하는 핵심 정보
양면 전기접점 제작에서는 접점 단품 도면과 리벳팅 후 조립 도면을 연결하는 것이 중요합니다. 단품 도면은 소재와 전면 머리, 다리 형상을 정의하고, 조립 도면은 후면 접촉면과 가동편의 기능 관계를 정의합니다. 후면 외경만 표시하기보다 접촉 높이·면 방향·위치 기준·허용 변형을 함께 정해야 의도한 접촉 기능을 재현할 수 있습니다.
| 전달할 정보 | 포함할 내용 | 설계·제작에서의 목적 |
|---|---|---|
| 접점 재료와 구조 | 솔리드·복합 구성, 앞뒤 기능 재료, 공급 상태 | 성형성·접촉 특성·재료 연속성 확보 |
| 가동편 조건 | 재질·판두께·구멍·기준면·표면 처리 | 삽입·체결·탄성 기능 연결 |
| 완성 후 기능 치수 | 앞뒤 높이·접촉면 방향·위치·가동편 휨 | 상대 접점과의 작동 관계 재현 |
| 전기·기구 조건 | 부하 유형·통전·개폐·접촉력·작동 변위 | 재료 선정과 기능 검증 범위 설정 |
| 검사와 이력 관리 | 치수·체결·전기·내구 판정 및 변경 관리 | 반복 생산 품질과 추적성 확보 |
설계 검토의 중심은 뒤쪽을 얼마나 크게 퍼뜨리는지가 아니라, 체결을 유지하는 형상과 전류를 안정적으로 전달하는 접촉면을 같은 공정에서 함께 만드는 것입니다. 전면 접점, 뒤쪽 성형면, 프레스 가동편을 따로 완성하는 부품으로 보지 않고 서로 영향을 주는 기능 구조로 다루어야 합니다.
아이디메탈의 전기접점·프레스 부품 제작을 검토할 때는 접점 도면과 가동편 도면, 조립 후 요구 형상, 사용 조건을 함께 전달하면 재료 배치와 공정 방향을 구체적으로 논의할 수 있습니다. 앞뒤의 접촉 역할과 검사 기준이 분명할수록 리벳팅 체결과 양면 접촉 기능을 일관되게 연결하기 수월합니다.
Double-Sided Electrical Contacts: Riveting Retention and Rear-Face Forming
A double-sided electrical contact uses its projecting shank to form a rear head that both fastens the contact to a blade and serves as a second working contact face. Stable operation on both sides requires coordinated control of material placement, shank flow, blade distortion, contact height and electrical verification.
The small joint connecting the contact to the stamped blade performs two jobs at once: mechanical retention and electrical contact. Its assembly quality therefore becomes part of the contact’s operating quality.
01Two contact faces completed by riveting
A double-sided electrical contact combines a preformed head on one side of a contact blade with a shank extending through the blade. Upsetting that projecting shank spreads its material into a secondary head. The new head both retains the blade and provides the contact face for the opposing stationary contact. The rear riveted shape is also an electrical working surface, which distinguishes this construction from a rivet used only for fastening.
The front head arrives with its contact geometry already formed; the rear head acquires its working geometry during assembly. Neither an acceptable front head nor a broadly spread tail is sufficient on its own. The process must preserve the front face, establish the rear height, diameter and surface condition, and retain the blade’s flatness and spring behavior.
| Feature | Mechanical role | Electrical role |
|---|---|---|
| Front contact head | Initial location and support during forming | Contact with one opposing stationary contact |
| Through-shank | Connection through the hole and material supply for upsetting | Part of the current path between the head and blade |
| Upset rear head | Retention of the contact in the blade | Contact with the opposite stationary contact |
| Stamped contact blade | Contact position, operating displacement and contact force | Current path from the external connection to the contact |
In a changeover mechanism, blade movement can bring each face into contact with a different stationary contact. The mechanism and circuit determine the actual switching sequence. A double-sided contact does not, by itself, establish simultaneous conduction or a double-break switching function.
02Material placement for a functional rear contact
A rear head can serve as a contact face only when the required contact material is present at that location. In a solid contact, the head and shank are made from the same contact material, so upsetting the shank still leaves that material at the rear surface. The two faces can nevertheless differ in hardness and surface condition because they have undergone different forming histories.
A conventional single-sided clad contact places the precious-metal contact layer at the head, while the remaining body and shank are generally copper or a copper alloy. Upsetting that shank exposes the shank material at the rear. It does not automatically create a silver contact layer or reproduce the switching performance of the front face. Rear-face use therefore requires a deliberate choice of material and opposing contact combination.
Construction options and the formed contact layer
| Material construction | Rear-face check after upsetting | Design priority |
|---|---|---|
| Solid contact | Formability, work hardening and cracking of the contact material | Balance contact performance with assembly formability |
| Single-sided clad contact | Suitability of the exposed shank material for rear contact service | Separate the front contact layer from the rear function |
| Composite contact with contact material at both ends | Continuity and remaining thickness of the rear functional layer | Design material placement together with material flow |
Double-sided composite designs can place contact material at the head and shank end, with a copper-based middle section. The decisive check is not only the original material cross-section, but which material remains at the working rear contact area after the secondary head has been formed, and whether it remains continuous.
Silver-based materials such as AgCu and AgNi vary in formability and contact behavior with composition, material structure and processing condition. A material name alone cannot define the forming load or final geometry. Material selection for the electrical duty must be connected to a process capable of forming a stable rear head.
03Shank projection and preparation of the blade hole
The projecting shank supplies the material for the rear head. Insufficient projection can prevent the process from achieving both the required working height and retention geometry. Excessive projection can demand large deformation and lead to unstable spreading. Shank length must account for blade thickness, material entering the hole and the intended rear-head shape.
The blade hole is part of the forming system. Its fit with the shank affects insertion, initial coaxial alignment, hole filling and joint clearance. An out-of-round hole or a rough fracture zone can tilt the shank or produce uneven flow. Burrs around the hole can prevent proper seating of the original head and transmit an uneven load into the blade.
| Controlled feature | Assembly effect | Verification |
|---|---|---|
| Shank length and projection | Rear height, diameter and forming allowance | Check incoming dimensions and projection in the assembled blade |
| Blade thickness | Variation in available projection and retention geometry | Measure local thickness and its variation |
| Hole size, roundness and location | Insertion, alignment and local material flow | Check the hole relative to functional locating features |
| Burrs, sheared edges and contamination | Poor seating, scratching and variation in joint resistance | Inspect both edges and the mating interface |
Stamping and contact assembly should be assessed as connected processes. Even a correctly located hole can be misaligned with the tooling if the blade remains warped. The assembly fixture must reproduce the blade datum and contact location, rather than merely hold the part in place.
04The insertion, support, forming and release sequence
Assembly of a double-sided contact follows four linked stages: insertion, support of the original head, rear-head forming and inspection after unloading. Protecting the finished front contact face is the starting point. The supporting die must match the head geometry, provide adequate stiffness and avoid indentation or angular distortion of the working face.
| Stage | Primary control | Subsequent check |
|---|---|---|
| Insertion and location | Shank-to-hole alignment and front-head seating | Lift, tilt and shank projection |
| Front-head support | Matching support geometry and clean tooling | Face impressions and uneven support |
| Rear upsetting | Defined deformation path and tool alignment | Rear height, diameter, eccentricity and cracks |
| Release and ejection | Removal of fixture load and elastic recovery | Blade warp, contact position and residual play |
Axial pressing, orbital riveting and other forming methods are selected to suit the material and assembly. Orbital riveting progressively moves the tool contact region and is used as an option for reducing deformation of thin contact blades. It requires suitable support against lateral force. Composite contacts also require verification of the interface between the functional material and supporting body. A lower forming force does not, by itself, establish freedom from cracking or delamination.
A component that appears flat under the forming tool can warp after unloading because of residual stress. The tool position at the end of the stroke therefore cannot be the only acceptance measure. Contact height and blade geometry should be inspected after release in a defined, stable condition.
05Material flow and control of the secondary head
Upsetting shortens the shank axially and drives plastic flow outward. As the rear head spreads, some material may enter the hole or spaces between the contact and blade. The same initial projection and tool travel can therefore produce different final heights and diameters when material hardness, friction, hole conditions or tool geometry change.
The available shank volume establishes the starting material supply, while the process determines the flow path. Checking only the outside diameter can miss a thin edge or a depressed center. The central working face and the surrounding retention region should be assessed together through height, cross-sectional shape, eccentricity and material continuity.
Variables governing rear-head formation
| Influence | Observable change | Control approach |
|---|---|---|
| Material hardness and processing history | Changes in forming load and spreading | Connect incoming condition with forming results |
| Tool alignment and contact conditions | Eccentricity, tilted head or local thinning | Check tool axis against fixture datums |
| Friction and surface condition | Uneven flow or surface tearing | Control lubrication, cleanliness and tool wear |
| Forming displacement and available shank material | Changes in contact height, diameter and retention | Review geometry together with the load history |
In a composite contact, material flow also changes the distribution of the functional layer. Material at the shank end can become locally thin or shift toward an edge as the head expands. A visually flat surface does not establish an acceptable material arrangement. Development-stage cross-sections help connect the completed geometry with the distribution of the working layer.
Arrow keys change the view
After tool release, a functional face remains on each side. Rear height, flatness and cracking are checked together with indentation of the front face.
Rear shank upsetting creates the fastening head and the second contact face in one forming operation
06Tooling that protects the front and forms the rear face
The front support die and rear forming tool should be designed as a pair. The first reacts the riveting load and limits distortion of the original head; the second establishes the geometry and height of the new working face. Small particles or damage on the support surface can imprint onto the finished front face, making tooling condition and cleaning part of product quality.
Rear-face flatness and angular orientation depend on the relationship between tool shape, tool axis and the blade datum. A tilted face can touch the opposing contact at one edge first. This shifts the contact mark and can increase variation in the actual contact area. Face orientation and location therefore deserve attention alongside outside diameter.
| Tooling or fixture feature | Purpose | Inspection focus |
|---|---|---|
| Support for the original head | Protect the existing contact face and geometry | Shape match, impressions and contamination |
| Rear forming surface | Produce contact height and working-face geometry | Wear, pickup and transferred surface marks |
| Tool-axis alignment | Limit eccentricity and uneven spreading | Relationship to the shank axis and blade hole |
| Local blade support | Control deformation of the surrounding sheet | Support position, flatness and post-release warp |
If the rear face requires a subsequent finishing operation, its material removal must be included in the original material layout. Excessive removal from a composite contact can change the material exposed at the working surface. Forming, finishing, cleaning and final inspection should be linked in one process specification.
07Retention that preserves blade flatness and spring behavior
A wider upset head does not automatically produce a better joint. Excessive deformation can pull or compress the sheet around the hole and distort the blade. Inadequate seating can leave small movements or tilt that destabilize the operating position and current path. The process window must satisfy both retention and contact functions.
A stamped contact blade often acts as a spring as well as a carrier. Even small local deformation near the rivet can alter its overall orientation and change contact force or changeover position in the assembly. This is why contact height and operating displacement should be checked relative to the blade’s functional datums, in addition to basic outline inspection.
Forming force, retention performance and operating contact force describe different properties. Forming force plastically deforms the shank during assembly. Retention performance describes how securely the completed contact remains in the blade. Contact force is the force against the opposing contact during operation, determined by spring behavior and mechanism displacement. A high forming force should not be interpreted directly as high contact force or low contact resistance.
| Insufficient or excessive condition | Potential effect | Functional check |
|---|---|---|
| Insufficient head seating | Micro-movement, rotation or variable joint resistance | Retention stability and path resistance |
| Excessive deformation around the hole | Blade warp or local damage | Free-state flatness and assembled position |
| Contact eccentricity or tilt | Edge contact or an uneven contact mark | Alignment with the opposing contact |
| Change in blade spring behavior | Variation in contact force or operating displacement | Force and position in each operating state |
Pull, push-out and rotational resistance tests are selected according to the joint and its service loads. Their results describe different properties. A destructive retention result cannot replace electrical contact assessment. Mechanical retention and electrical function should be connected within the qualification plan while keeping their acceptance criteria distinct.
08Cracks, folds and surface condition of the upset face
The rear head is a working surface that has undergone substantial plastic deformation. Edge cracks, folded material, tearing, tool marks and forming residue can affect the contact location and current path as well as appearance. Small edge cracks can be missed in a top view, so side surfaces and transitions should also be inspected.
A visually smooth face is not necessarily an electrically stable face. Surface films and organic residue can cause resistance variation in low-energy signal contacts, while adhered particles can change contact marks and local load distribution. When forming lubrication is required, cleaning and handling must be compatible with the final contact-surface requirements.
| Inspection target | Technical significance | Further check |
|---|---|---|
| Cracks at the rear-head edge | Possible limit in formability or material condition | Magnified examination and cross-sectioning where needed |
| Folds, laps or surface tearing | Unstable material flow or surface damage | Compare tooling condition and process settings |
| Functional-layer discontinuity or exposed substrate | Change in the material at the working contact area | Check material distribution and cross-section |
| Oil, particles or discoloration | Change in the contact-interface condition | Cleanliness and electrical-function checks |
Plating or other surface treatment is a separate design decision. Forming pre-plated material requires examination of the coating in the strained region; plating after forming requires review of final dimensions and face condition. A thicker coating or a brighter finish cannot repair an underlying forming defect or an inadequate joint.
09Front and rear working height and contact force
A double-sided contact is one component with two distinct working conditions. Front and rear heights, blade location, and the height and orientation of each stationary contact combine to determine touch position and overtravel. Variation in rear-head height can change the force on one side even when mechanical retention remains adequate.
Contact force is not distributed uniformly across the entire visible face. Current flows through microscopic contact spots influenced by roughness, films, material and load. Increasing the apparent head area is therefore different from establishing a stable real contact area. Contact force and face alignment must be considered together.
| Feature assessed on each side | Purpose | Related conditions |
|---|---|---|
| Working-face height and location | Establish contact at the intended operating position | Blade and stationary-contact datums |
| Face angle and contact mark | Identify uneven or edge contact | Mechanism alignment and blade orientation |
| Contact force and overtravel | Maintain conduction and operating margin | Spring behavior and assembly tolerances |
| Open gap and changeover position | Confirm the intended switching sequence | Drive displacement and circuit configuration |
Even when both faces use the same material, different operating frequencies or switching duties can produce different rates of wear and surface change. Similar initial resistance on the two sides does not establish identical behavior throughout service. Each face should be assessed under its own operating conditions.
Arrow keys change the view
The moving blade passes through an open position. Contact sequence and clearance are established by the actual switching mechanism.
The two faces of one moving contact engage their respective fixed contacts
10Conduction, temperature rise and switching durability
The voltage drop in a conducting assembly includes contributions from the mating contact interface, contact body, connection to the blade and the blade itself. Increased resistance in one region can increase local heating, while rising temperature can in turn influence contact force and surface condition. Conductivity of the contact material alone therefore does not describe the electrical quality of the assembly.
During switching, assessment extends beyond contact resistance to bounce, arcing, material transfer, erosion and possible welding. These behaviors depend on AC or DC duty, load characteristics, operating speed, opening gap, contact force and opposing contact material, as well as voltage and current. Material selection and rear-head geometry should be evaluated within the intended mechanism and electrical duty.
| Operating condition | Key observations | Evaluation focus |
|---|---|---|
| Low-energy signal contact | Resistance stability and variation | Effects of films, particles and contact force |
| Continuous conduction | Voltage drop and temperature rise | Separate complete-path behavior from local heating |
| Repeated switching | Bounce, erosion, material transfer and welding | Use representative loads and operating conditions |
| Long-term use and environmental exposure | Changes in resistance, force and surface condition | Assess mechanical, thermal and environmental influences together |
Good welding resistance in the material cannot compensate for insufficient contact force or excessive mechanism bounce. Equally, a strongly retained contact can still perform poorly if the conducting interfaces are unstable. Material, riveting quality, blade behavior and mechanism conditions should be validated as one operating system.
11Inspection of both faces and the retained joint
Separating front-face contact performance, rear-face contact performance and retention in the blade reduces inspection gaps. A single combined test can mix joint resistance with mating-contact resistance or allow the condition of one face to obscure a defect on the other.
Electrical resistance measurement begins with defined connection points and a defined current path. Four-wire measurement reduces lead influence, but the blade, retained joint and mating interface located between the sensing points still contribute to the result. Distinguish complete-path measurements from measurements of a particular region. When comparing the two faces, control probe material and position, contact force and loading history. For low-energy contacts, the test current and voltage should avoid unintentionally altering the surface film under investigation.
| Inspection group | What is assessed | Conditions to record |
|---|---|---|
| Geometry | Front and rear heights, diameters, angles and blade warp | Datum system and unloaded condition |
| Surface and material | Cracks, folds, functional-layer distribution and residue | Observation location and method |
| Retention | Play, rotation and retaining capability | Load direction, support and acceptance criteria |
| Electrical | Resistance, voltage drop and heating on each side | Measurement points, force, current and duration |
| Operating durability | Resistance, wear and force changes after switching | Load, operating speed and assessment intervals |
During development, cross-sectioning and destructive tests can establish the relationship between external geometry and internal condition. Production control can then combine repeatable non-destructive dimensional, visual and electrical inspections with process monitoring. Inspection scope and frequency should reflect failure consequences and process variation rather than a universal checklist.
12Process control linked to finished-contact quality
Identical machine settings do not guarantee identical results when incoming material and component conditions change. Recording contact material condition, blade thickness, hole quality, tool wear and fixture cleanliness alongside finished dimensions improves traceability. Rear contact height deserves particular attention because it is both a joint dimension and a functional mechanism dimension.
Where the equipment supports it, force-displacement monitoring can help detect incorrect insertion, changes in available material or abnormal forming resistance. A trace within an established range does not guarantee surface cleanliness or the condition of an internal functional layer. Monitoring limits become useful when correlated with actual dimensions, sections and functional results.
Process records and finished-part quality
| Process control item | Related result | Check when changed |
|---|---|---|
| Contact material lot and processing condition | Forming load, cracks and face condition | Compare forming and electrical behavior before and after the change |
| Stamped-blade lot | Projection, blade warp and contact position | Thickness, hole and surface condition |
| Tool life and maintenance | Height, eccentricity and transferred marks | First-off parts and repeatability after replacement |
| Forming settings and fixture condition | Joint shape, play and electrical variation | Change history and functional verification |
Classifying a defect only by its appearance on the rear face can hide a problem with front support or the stamped hole. The surface showing a symptom may differ from the process where the cause originated. Linking front and rear images, dimensions, forming records and inspection results to the same component identification supports more effective investigation.
Linked inspection of contact faces, fastening and the moving blade
13Information that completes the drawing and inspection plan
Double-sided contact manufacturing requires a link between the individual contact drawing and the riveted assembly drawing. The first defines the material, original head and shank; the second defines the functional relationship between the formed rear face and the blade. Rear diameter alone is insufficient. Working height, face orientation, position datums and allowable blade deformation should also be defined.
| Information to provide | Required content | Purpose in design and manufacturing |
|---|---|---|
| Contact material and construction | Solid or composite structure, materials on both working faces and supply condition | Establish formability, contact behavior and material continuity |
| Blade requirements | Material, thickness, hole, datum surfaces and finish | Connect insertion, retention and spring function |
| Completed functional geometry | Front and rear heights, face orientation, position and blade warp | Reproduce the relationship with opposing contacts |
| Electrical and mechanism duty | Load type, conduction, switching, force and operating displacement | Define material selection and validation scope |
| Inspection and traceability | Dimensional, retention, electrical and durability acceptance with change control | Support repeatable production and traceability |
The central design objective is not simply to spread the tail as widely as possible. It is to create a retaining geometry and a stable current-carrying working face in the same operation. The original head, formed rear face and stamped blade must be treated as an interacting functional structure.
For discussions with ID METAL about electrical-contact and stamped-component manufacturing, provide the contact and blade drawings together with the required assembled shape and operating conditions. Clear roles for both contact faces and clear inspection criteria make it easier to connect riveting retention with reliable double-sided contact function.
전기접점·프레스 부품 제작 문의
추가 정보
검색엔진용 요약
양면 전기접점은 접점 다리를 가동편 뒤쪽에서 리벳팅해 체결하고, 성형된 뒤쪽 머리를 두 번째 접촉면으로 쓰는 부품입니다. 후면 접촉 기능은 재료 배치·다리 돌출량·금속 유동·공구 정렬로 정해지므로, 앞뒤 접촉 높이와 면 방향, 가동편 평탄도, 체결 안정성, 각 면의 전기 저항을 하중을 해제한 완성 상태에서 확인합니다.
핵심 포인트 정리
- 후면 머리는 가동편을 붙잡는 체결부이면서 반대쪽 상대 접점과 닿는 접촉면입니다.
- 일반적인 단면 클래드 접점의 다리를 성형하면 후면은 다리 재료의 표면이 되며, 은계 접촉층이 자동으로 생기지 않습니다.
- 솔리드 접점이나 양단에 접점 재료를 둔 복합 구조로 후면 접촉 기능을 설계하고, 성형 뒤 실제 접촉 위치에 남는 재료를 확인합니다.
- 다리 돌출량은 판두께·구멍 채움량·목표 후면 형상을 함께 보고 정하며, 구멍의 크기·진원도·버도 공정의 일부로 관리합니다.
- 앞면 지지 공구와 후면 성형 공구는 한 쌍으로 설계하며, 지지면의 이물이나 손상은 앞면 접촉면에 전사될 수 있습니다.
- 후면을 크게 퍼뜨릴수록 체결이 좋아지는 것은 아니며, 과도한 변형은 가동편 휨과 접촉력 변화를 만들 수 있습니다.
- 성형 하중, 체결 유지 성능, 사용 중 접촉력은 서로 다른 항목이므로 각각 합격 기준을 둡니다.
- 완성 치수는 가압 중이 아니라 하중을 해제한 상태에서 앞뒤 높이·면 방향·가동편 형상으로 판정합니다.
FAQ
양면 전기접점은 일반 체결용 리벳과 무엇이 다른가요?
일반 체결용 리벳의 뒤쪽 머리는 고정 역할을 하지만, 양면 전기접점의 뒤쪽 성형 머리는 반대편 고정접점과 맞닿는 접촉면이 됩니다. 그래서 후면의 높이·외경·면 상태를 체결 형상이 아니라 접촉 기능면으로 관리합니다.
클래드 접점으로도 양면 접점을 만들 수 있나요?
일반적인 단면 클래드 접점은 머리의 접촉층에 귀금속 재료를 쓰고 다리는 동 또는 동합금으로 구성합니다. 뒤쪽을 성형해도 후면은 다리 재료의 표면이므로, 후면을 전기접점으로 쓰려면 그 재질과 상대 접점의 조합을 따로 선정하거나 양단에 접점 재료를 둔 구조를 검토합니다.
양면 접점은 앞뒤가 동시에 통전되나요?
그렇지 않습니다. 전환형 기구에서는 가동편이 움직이면서 앞면과 뒷면이 각기 다른 고정접점에 닿을 수 있고, 통전 순서와 개폐 기능은 기구와 회로 구성으로 정해집니다. 양면 구조만으로 동시 통전이나 이중 차단 기능이 생기지는 않습니다.
다리 돌출량은 어떻게 정하나요?
가동편 판두께, 구멍 안으로 채워지는 양, 목표 후면 형상을 함께 고려합니다. 돌출량이 부족하면 접촉 높이와 체결 형상을 함께 확보하기 어렵고, 과도하면 큰 압축 변형과 불안정한 퍼짐이 생길 수 있습니다.
궤도 리벳팅을 쓰면 가동편 변형이 없어지나요?
궤도 리벳팅은 공구가 닿는 영역을 순차적으로 옮기며 성형하는 방식으로, 얇은 접점 가동편의 변형을 줄이기 위한 선택지입니다. 측방력을 받는 지지가 필요하고, 복합 접점은 기능층과 몸체 사이 계면도 확인해야 합니다. 하중이 낮다는 이유만으로 균열과 박리가 방지된다고 판단하지 않습니다.
후면 머리의 외경만 맞으면 합격인가요?
외경만 보면 가장자리가 얇아지거나 중앙이 오목해진 상태, 기울어진 접촉면을 놓치기 쉽습니다. 접촉 높이·면 방향·편심·가장자리 균열과 가동편 휨을 함께 확인합니다.
앞뒤 접촉면의 전기 저항은 어떻게 검사하나요?
측정점과 전류 경로를 먼저 정합니다. 4선식 측정은 리드의 영향을 줄이지만 감지점 사이의 가동편·체결 계면 저항은 결과에 포함되므로, 전체 경로의 값인지 특정 구간의 값인지 구분하고 프로브 위치·접촉력·하중 이력을 일정하게 관리합니다.
양면 접점 제작을 검토하려면 무엇을 준비하나요?
접점 단품 도면과 리벳팅 후 조립 도면, 접점 재료와 구조, 가동편의 재질·판두께·구멍, 앞뒤 접촉 높이와 면 방향 같은 완성 후 기능 치수, 전기·기구 조건과 검사 기준을 함께 준비하면 검토가 구체화됩니다.
관련 주제 확장 설명
업세팅과 금속 유동
업세팅은 다리를 축 방향으로 줄이면서 재료를 옆으로 이동시키는 소성가공입니다. 같은 돌출 길이와 공구 이동량이라도 소재 경도·마찰·구멍 조건·공구 형상에 따라 최종 높이와 외경이 달라지고, 복합 재료에서는 기능층 분포까지 바뀌므로 개발 단계에서 단면으로 확인합니다.
성형 하중·체결 유지 성능·접촉력의 구분
성형 하중은 조립할 때 다리를 소성변형시키는 힘이고, 체결 유지 성능은 조립 후 접점이 가동편에 안정적으로 유지되는 특성이며, 접촉력은 작동 중 상대 접점을 누르는 힘입니다. 큰 성형 하중을 높은 접촉력이나 낮은 접촉 저항으로 해석하지 않습니다.
하중·변위 이력과 공정 추적
장비가 지원하면 하중·변위 이력으로 잘못된 삽입, 재료량 변화, 비정상적인 성형 저항을 찾을 수 있습니다. 다만 정상 범위의 파형이 표면 청정도나 기능층 상태까지 보증하지는 않으므로, 치수·단면·기능 검사와 연결해 관리 한계를 정합니다.
내부 링크
전기접점과 정밀 프레스 가공 사업분야에서 제품군을 확인할 수 있습니다. 함께 볼 글은 튜블라 전기접점 리벳팅, 리벳 접점 조립품, 솔리드 접점과 클래드 접점의 차이, AgNi·AgCu 전기접점 재질 비교, 접점 용착과 발열입니다. 양면 접점과 가동편 조립 검토는 도면과 사용 조건을 첨부해 제품문의·개발의뢰로 전달해 주세요.